If you’ve ever visited a steel mill, you know the reheating furnace is the beating heart of the billet prep process. It’s where cold steel billets get heated to a precise temp—usually between 1100°C and 1250°C—so they can be rolled, forged, or shaped without cracking. But let’s be real: messing with the control panel here is no casual task. As a guy who’s spent over a decade selling, installing, and fixing these furnaces (I’ve worked with every make, from small 1-ton units to 100-ton industrial giants), I’ve seen what happens when operators cut corners. Last year, a mill near me fried a $20k burner because their crew ignored a simple panel step. Another once shut down for 12 hours because they flipped a valve wrong. Steel Billet Reheating Furnace
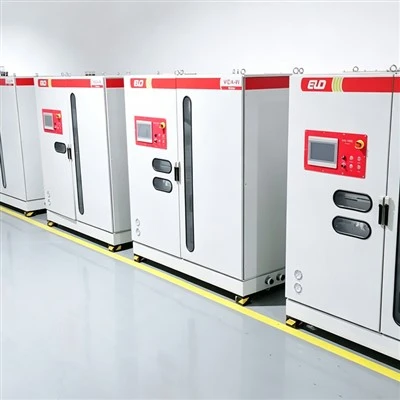
This post isn’t for newbies who just unboxed their first furnace. It’s for the guys in the control room who grab their coffee, log in, and actually run the show. I’m gonna break down the panel moves you can’t skip, the mistakes everyone makes, and the little hacks I’ve picked up from years on the job. No fancy jargon—just the stuff that keeps your line moving and your furnace alive.
First, let’s start with the basics you probably skim over: what the control panel even is. For most modern reheating furnaces (not those rickety old ones with analog dials), your panel has 4 core sections. Don’t laugh—if you don’t know these, you’re gonna mess up. 1) The HMI (human-machine interface) screen: this is your dashboard, shows temp zones, fuel pressure, oxygen levels, all that good stuff. 2) The fuel system controls: burners, gas valves, pressure regulators. 3) The combustion safety interlocks: these are the built-in failsafes—if something’s off, the panel locks you out until you fix it. 4) The production schedule tab: where you input how many billets you’re heating and how fast they move.
I’ve had operators come to me going, “The HMI is broken, won’t let me start.” 9 times out of 10, it’s because they skipped pre-checking the safety interlocks before logging into the schedule. Let’s walk through the startup sequence step-by-step because this is where 70% of mess-ups happen.
First, pre-start check. Before you even touch the panel, walk around the furnace’s control skid (the metal box where all the wiring and valves sit). Check if the natural gas pressure is at the right level—usually 3-5 PSI for small units, up to 10 PSI for big ones. If it’s too low, your burners won’t light; too high, you’ll get a flashback. Next, open the vent valve on the furnace roof for 5 minutes. Old furnaces trap gas in the chamber, and if you light the burner without venting, you’ll get a small explosion. I’ve seen this: a guy last month thought the vent was a “waste of time” and his burner blew out the side of the housing—no injuries, but $5k in repairs. Don’t be that guy.
Back to the panel. First, log into the operator account—never use the admin account. That’s a big rule. Admin is for changing temp setpoints or updating firmware, not for daily starts. Once you’re logged in, the first screen you’ll see is the “System Status” tab. Scan this for red warnings before you do anything. Common red flags: oxygen level too high (over 8%) or too low (under 2%), fuel pressure below threshold, door interlock fault (if the furnace door’s not closed tight, the panel won’t let burners fire). If you see a red fault, don’t hit “reset” right away. That’s the second biggest mistake. I’ve watched operators hammer the reset button, and instead of fixing the oxygen level, they just triggered a gas leak. If there’s a fault, go into the “Fault Log” tab (it’s usually a small icon on the HMI, labeled “Logs”) to see what’s actually wrong. Most of the time, it’s a simple fix: oxygen sensor is dirty, so you just pull it out and wipe it with a cloth. Or the door interlock switch got bumped—jiggle it, and it clears.
Now, let’s get to the burner startup. Once all red faults are gone, go to the “Burner Control” tab. Here’s where you choose between manual and auto mode. Auto mode is great for routine runs—set your temp zones (I’ll explain that in a sec) and the panel does the work. But new operators love to jump straight to auto without checking manual mode first, and end up with uneven heating. For manual startup (which you should do once a week to calibrate the burners, by the way), start with the pilot light. Don’t turn the main gas valve on first. The HMI will have a “Pilot Ignition” button—hold it for 10 seconds (not 5, I’ve tested this: 5 is too short, the pilot goes out) until you see a green “Pilot Lit” light. Then, turn on the main gas valve, and slowly open the burner’s fuel valve. If you crank it open all at once, you’ll get a flame that’s too big, which can overheat the billet edges and cause scale (that’s the flaky rust you don’t want—too much scale means lost material, wasted money).
Wait, temp zones: let’s talk about that. Most reheating furnaces have 3 zones: preheat, heating, and soaking. Preheat is where cold billets go first—you want this zone at 700-800°C, so they warm up slowly and don’t crack from thermal shock. Heating zone is where you get to 1150-1200°C, the sweet spot for rolling. Soaking zone is where you hold the temp for 20-30 minutes, so every part of the billet is the same. Here’s a trick I tell all my clients: don’t set all zones to the same temp. If you do, the front of the billet will overheat while the back is too cold. The HMI will let you adjust each zone separately—use that. I’ve had a mill that set all zones to 1250°C, and they had to scrap 20 tons of billets because the ends were melted. Dumb, but avoidable.
Now, what if you need to stop the furnace? Not just an emergency stop, but a regular shutdown. Operators love to hit the big red E-stop button when they’re in a rush—don’t do that unless there’s a fire or a gas leak. E-stop cuts all power, and if you restart, you’ll have to go through the entire pre-start sequence again, which wastes 15-20 minutes. Instead, use the “Normal Shutdown” tab on the HMI. Here, you can set the furnace to ramp down temp slowly over 2 hours, which preserves the burners and sensors. Last year, a client of mine hit E-stop because a billet got stuck, and it took 3 hours to get back up. If they’d used normal shutdown, it would’ve been 45 minutes. Small move, big time savings.
Now, the most overlooked part of operating the panel: monitoring in real time. The HMI isn’t a set-it-and-forget-it screen. I tell my guys to check it every 15 minutes, not once an hour. What to look for? First, the oxygen level. If it drops below 4%, your burner is running rich, which means you’re wasting fuel and creating more scale. If it’s over 9%, you’re running lean, which can damage the burner’s nozzle over time. The panel will usually alert you, but don’t wait for the alert—check it yourself. Second, the billet exit temp. If that temp is too low, the rollers will slip; too high, you get bad shapes. I’ve seen operators just go by the zone temp, but the exit sensor (another part on the HMI) is what actually matters.
Now, the mistakes that come up again and again. Let’s list the top 5, because I hear these every week. 1) Ignoring interlocks: those safety switches are there for a reason. I had a guy who bypassed the door interlock so he could “speed up” production, and a billet fell out of the furnace—burned a worker’s arm, and the mill paid $50k in comp. Interlocks aren’t a hassle; they’re your safety net. 2) Forgetting to vent the furnace at startup: like I said earlier, gas buildup is a recipe for disaster. 3) Resetting faults without checking the log: that’s how you end up with gas leaks or burner failures. 4) Using auto mode for every run: auto is great for routine, but if you’re heating a different grade of steel (like stainless vs. carbon steel), you need to adjust the zones manually. Stainless needs a higher soak temp, for example. 5) Skipping weekly burner calibrations: once a week, switch to manual mode, light the pilot, and check the flame. It should be blue, not yellow. A yellow flame means incomplete combustion, wasting fuel. Just turn the air valve on the burner until the flame turns blue—takes 2 minutes, saves hundreds a month on gas.
Wait, what about if the HMI glitches? I’ve had this happen: the screen goes black, or a temp reading is way off. First, check the wiring to the sensor—most of the time, it’s a loose wire, not a broken panel. If that’s not it, turn the furnace to manual mode, and use the analog dials (if your panel has them) to control the burners. Don’t keep running it with a glitchy HMI—you’ll end up with bad billets, and if the temp is too high, you’ll damage the furnace’s refractory (the lining, which is super expensive to replace). I once had a client who ran with a bad HMI for a week, and they had to replace 100 sq ft of refractory—cost them $12k.
Now, let’s talk about who should operate this panel. It might seem obvious, but I still see mill crews letting new guys run the panel without training. You need someone who’s been through 20+ startup and shutdown cycles, knows how to read the fault log, and understands steel billet heating basics. I offer free 1-day training for all my clients, because I’d rather spend a day training a crew than a week fixing their mess after a mistake. If your guys are new, get them trained—no exceptions.
At the end of the day, running the reheating furnace control panel isn’t rocket science, but it’s not something to wing. It’s about following the steps, checking the small stuff, and not cutting corners on safety or maintenance. The good news is, most issues are preventable. A 5-minute pre-start check, scanning the HMI every 15 minutes, and fixing faults instead of resetting them—those moves will keep your furnace running smooth, your billets good, and your costs down.
If you’re looking to upgrade your reheating furnace control panel, or need replacement parts, or even just want a second opinion on your current setup, hit me up. I’ve been doing this for years, I know every make and model, and I can help you get the most out of your furnace. No sales pitch, just straight talk about what works for your operation.
Steel Plate Induction Heating Production Line References:
- Steel Industry Energy Conservation Association. Reheating Furnace Operational Best Practices, 2022.
- American Iron and Steel Institute. Reheating Furnace Safety Protocols, 2021.
- International Association for Steel Technology. Billet Heating Temp Guidelines, 2023.
Hebei Yuantuo Electromechanical Equipment Manufacturing Co., Ltd.
As one of the most professional manufacturers and suppliers of steel billet reheating furnace in China, our products have good reputation in the market. Please rest assured to buy advanced equipment made in China here and get quotation from our factory. Customized orders are welcome.
Address: Yanshan Street West and Jialingjiang Road North, Economic and Technological Development Zone, Wuqiao County, Cangzhou City, Hebei Province, China
E-mail: yuantuotech01@gmail.com
WebSite: https://www.yuantuoem.com/
